


Blog
- Deep litter layer system performance links clean eggs, stable flock management, and practical poultry equipment, with litter moisture targeted at 20–30% and efficient daily control.
Automatic layer poultry equipment supports consistent feeding, drinking, nesting, ventilation, and collection across commercial houses.
Automatic egg collection systems reduce unnecessary handling while supporting cleaner transfer from nest to packing area.
Proper ventilation equipment manages humidity, airflow, and house conditions while reducing moisture-related litter problems.
- A coordinated poultry equipment solution can connect production hardware with automated controls for more consistent commercial egg quality.
Get professional poultry farm construction guidance, equipment selection solutions, and the latest price lists, whatsApp to +8618830120193, click to learn more:
Why Egg Quality Matters In Deep Litter Systems
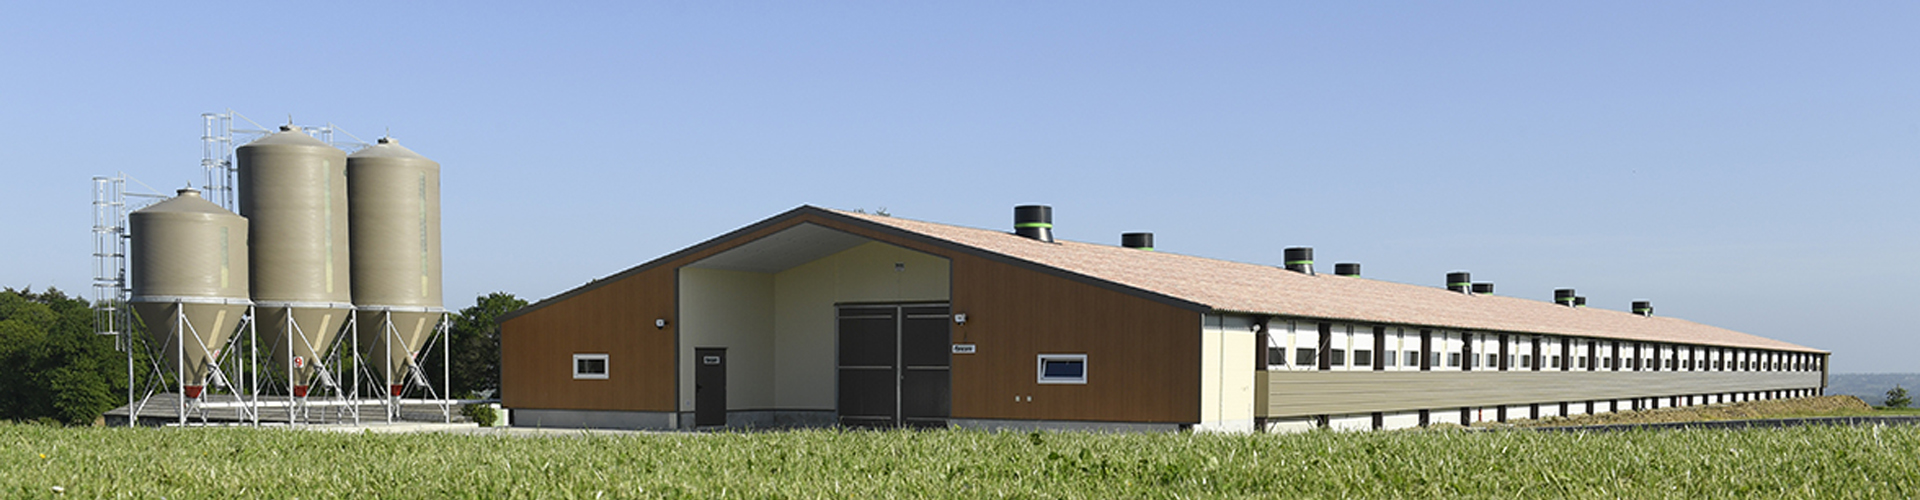
In deep-litter layer houses, egg quality depends on litter management, water delivery, nesting behavior, climate control, and collection procedures.
A well-engineered deep litter layer system combines automatic layer poultry equipment with automatic egg collection systems, while commercial projects can integrate sensors and controls for operating conditions around 20–30% litter moisture.
Keep The Litter Dry And Clean
Engineering Point
Water leakage is a direct cause of wet litter around drinking lines.
A properly engineered deep litter layer system with automatic layer poultry equipment should include pressure regulation, filtration, end-line flushing, and anti-drip components.
Stainless-steel drinkers provide durable construction for commercial houses operating through long production cycles.
Engineering Checklist
Use pressure regulators at each drinking circuit.
Install filters before nipple lines.
Provide flushing points at line ends.
Inspect nipple seals and connectors regularly.
Keep drinking lines accurately leveled.
Litter And Water Management Parameters
Data is for reference only.Swipe horizontally to view full table.
Provide Consistent Feed And Water
Uneven feed distribution can increase competition and create differences in body condition across the flock.
Automatic layer poultry equipment distributes feed through synchronized motors, augers, chains, or feed pans.
For a commercial deep litter layer system, equipment selection should match flock size, house geometry, feed characteristics, and programmed feeding frequency.
Technique Card
Objective: Create uniform access from the first feeder point to the final section.
Recommended Configuration
- Feed storage silo.
- Automatic hopper.
- Motor-driven feed line.
- Precision feed pans.
- Feed-level sensor.
Programmable control panel.
Feeding Equipment Technical Data
Data is for reference only.Swipe horizontally to view full table.
Improve Nesting Management
Floor eggs are exposed to litter, bird traffic, and repeated physical contact.
An automatic nest within a deep litter layer system provides a dedicated laying area and guides eggs away from the flock immediately after laying.
Roll-away structures and automatic egg collection systems create a controlled transfer route while reducing direct contact between eggs and litter.
Process Structure
Hen enters nest → Egg is laid → Sloped nest floor moves egg away → Egg reaches collection belt → Conveyor transfers egg → Central collection point receives egg
Nesting System Technical Comparison
Data is for reference only.Swipe horizontally to view full table.
Control Temperature, Humidity, And Airflow
Ventilation removes moisture generated by birds, litter, manure decomposition, and normal house activity.
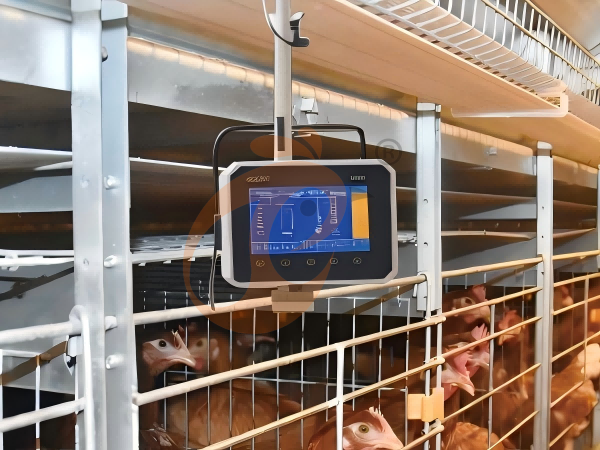
A commercial deep litter layer system can combine automatic layer poultry equipment with exhaust fans, adjustable air inlets, sensors, and controllers for more consistent environmental management.
Automated control allows ventilation output to respond to measured conditions and can reduce repeated manual adjustments.
Equipment Combination Recommendation
Variable-speed exhaust fans + adjustable air inlets + temperature sensors + humidity sensors + ammonia monitoring + climate controller
This equipment combination supports controlled airflow while connecting environmental monitoring with automatic poultry equipment operation.
Climate Control Technical Parameters
Data is for reference only.Swipe horizontally to view full table.
Reduce Egg Damage During Collection
Egg quality can be lost after laying when eggs experience repeated handling or poorly aligned transfers.
An automatic egg collection system integrated into a deep litter layer system creates a continuous route from nest to central collection.
The transfer section should use synchronized movement and controlled transitions, with each component selected around the project’s daily production volume.
Engineering Point
Use synchronized motors and adjustable conveyor controls according to actual flock output.
For larger commercial projects, automatic layer poultry equipment can centralize collection while reducing worker movement inside the poultry house.
Egg Handling Equipment Technical Data
Data is for reference only.Swipe horizontally to view full table.
Build An Integrated Egg Quality System
The five improvements work best when feeding, drinking, nesting, ventilation, and collection are engineered as one deep litter layer system.
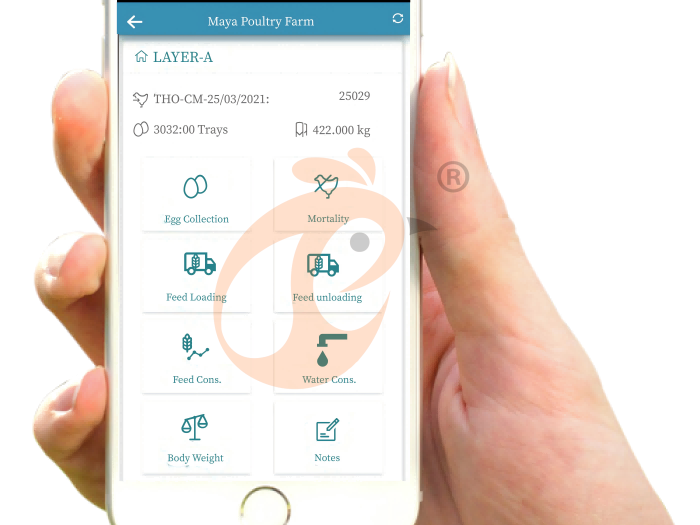
An integrated poultry equipment package can connect automatic layer poultry equipment, automatic egg collection systems, sensors, and control software into one operating structure.
The project layout should consider flock size, building dimensions, climate, labor availability, and expansion requirements.
The objective is controlled production, combining dry litter, consistent feed access, stable climate, protected nests, and gentle egg transportation.
Frequently Asked Questions
Q1: How does a deep litter layer system improve egg quality?
A deep litter layer system coordinates nesting, drinking, ventilation, and collection to reduce contamination opportunities, while 20–30% litter moisture provides a practical management reference.
Q2: Which equipment helps reduce floor eggs?
Automatic nest boxes integrated with an automatic egg collection system provide a dedicated laying route and move eggs away from birds and litter after laying.
Q3: Why is ventilation important for egg quality?
Ventilation equipment removes moisture and supports stable house conditions, while sensor-based control can monitor temperature within approximately ±0.3°C.
Taiyu (HK) Group - One Of China Toppest Deep Litter Layer System Manufacturer
Deep litter layer system engineering integrates automatic feeding, nipple drinking, nesting, ventilation, and egg collection, with project layouts engineered around commercial flock capacity.
Global factory-direct supply covers complete poultry equipment packages, including feeding lines, drinking systems, nests, ventilation units, conveyors, and control components.
Turn-key engineering supports house planning, equipment configuration, installation guidance, commissioning procedures, and production-line integration.
Project delivery can support international farms requiring coordinated equipment specifications, electrical control integration, water systems, and customized house layouts.
Factory manufacturing enables direct technical communication, equipment matching, spare-parts planning, and commercial project support for different poultry production capacities.
Contact Us To Received Your Customized Poultry Farm Plan
Headquarters And Branchs
Hong Kong Headquarter Management Team
Hong Kong Headquarter Taiyu Industrial Group CO., LTD
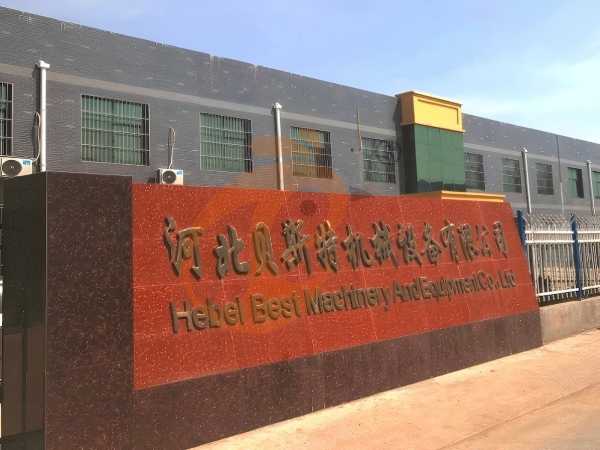
China Hebei Best Machinery And Equipment CO., LTD
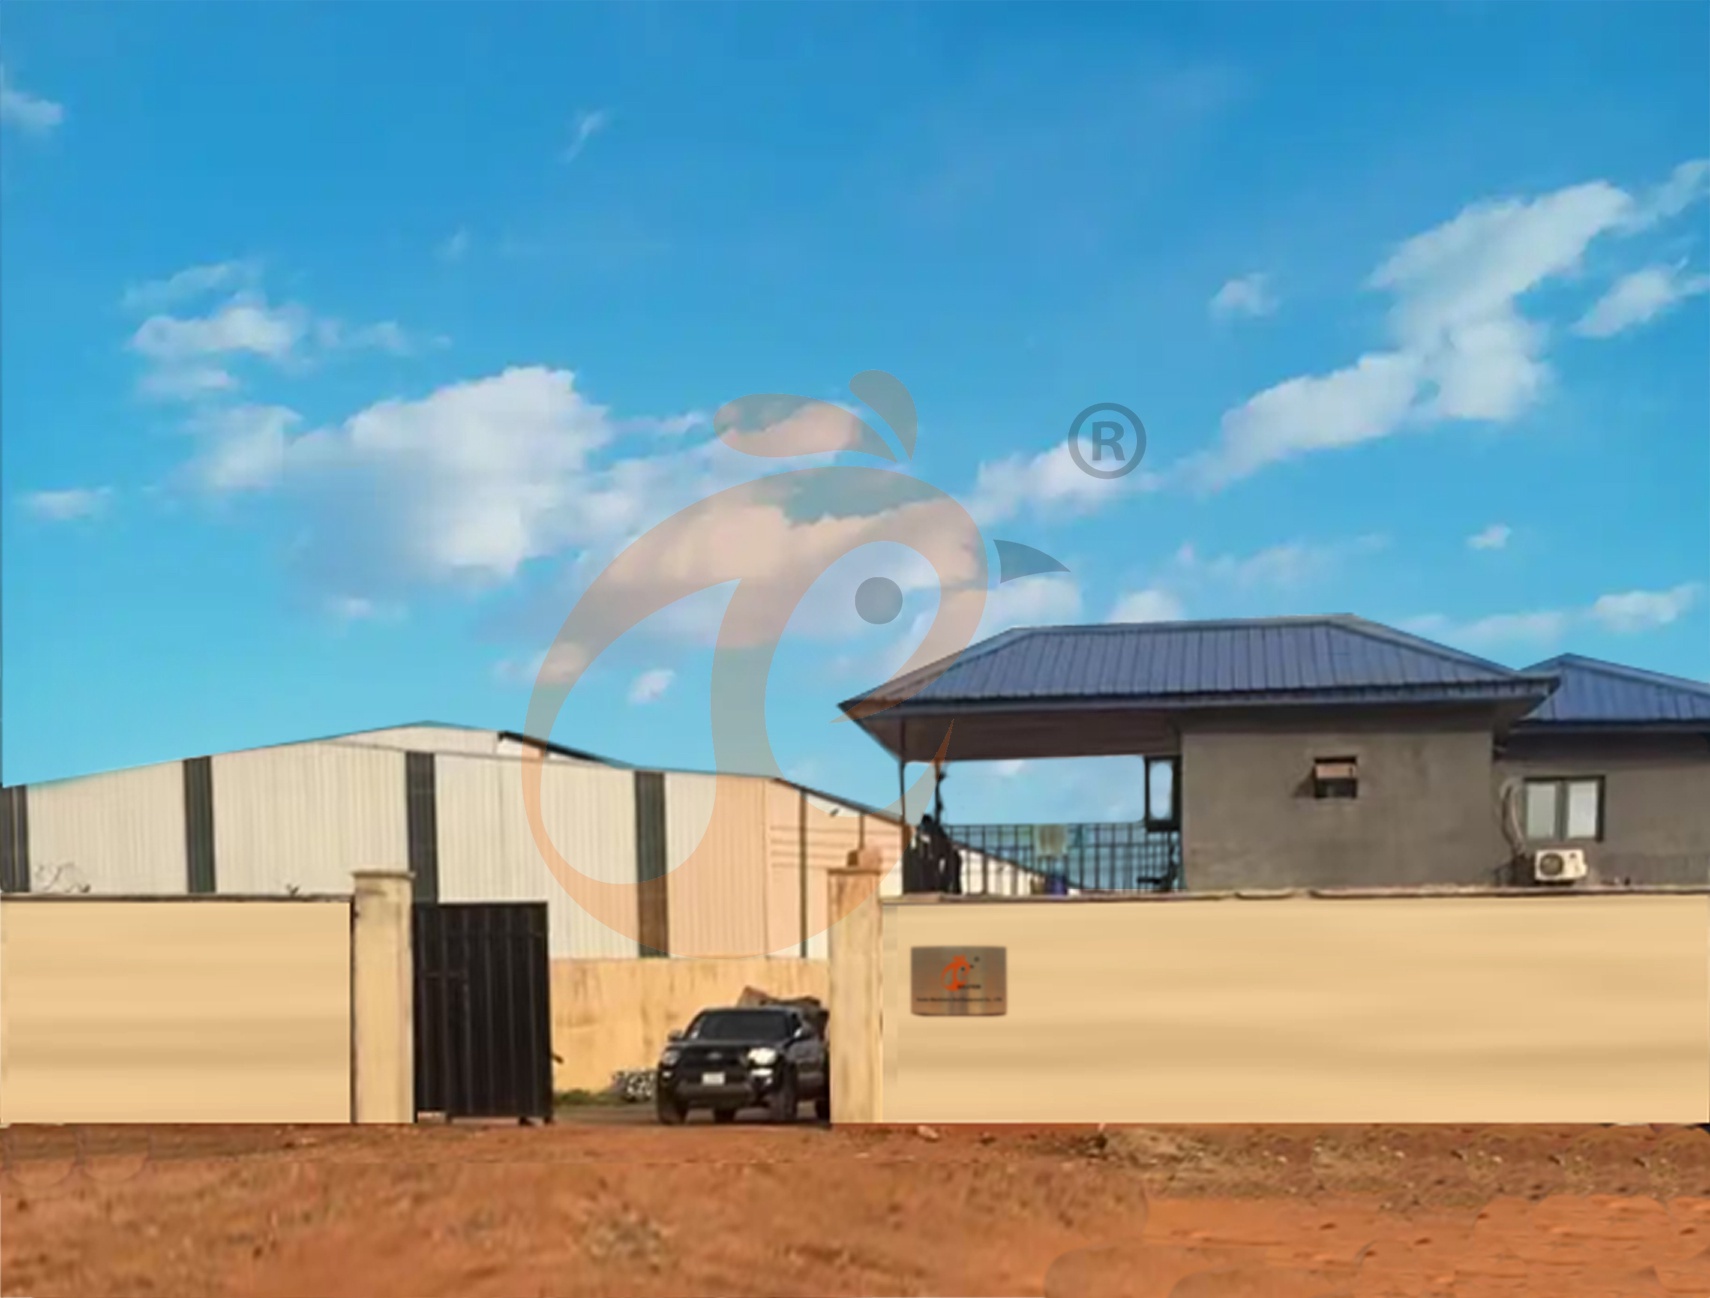
Nigeria Vanke Machinery And Equipment CO., LTD
Tanzania Best Machinery And Equipment CO., LTD
Ethiopia Best Hebei Machinery Manufacturing PLC
Reception /24 WhatsApp NO. : +8618830120193
FAQ
What Are The Growth Performance Benefits In Deep Litter Poultry System?
Feed conversion ratio improves to 1.55–1.78 due to thermal comfort and reduced stress.
Market uniformity rate exceeds 85%–92% within target slaughter weight range.
What Are The Litter Turning And Management Frequency Standards In Deep Litter Poultry System?
Surface leveling is maintained every 3–5 days to prevent compaction zones.
Full litter replacement cycle occurs every 2–3 production batches depending on load intensity.
What Are The Energy Efficiency And Cost Advantages In Deep Litter Poultry System?
Construction cost savings reach 25%–40% compared with fully caged housing systems.
Operational labor demand decreases by 30%–50% through simplified floor-based management.
Message
Products recommended
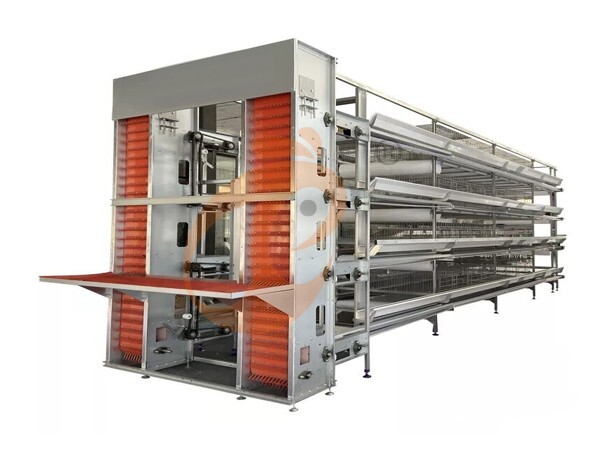
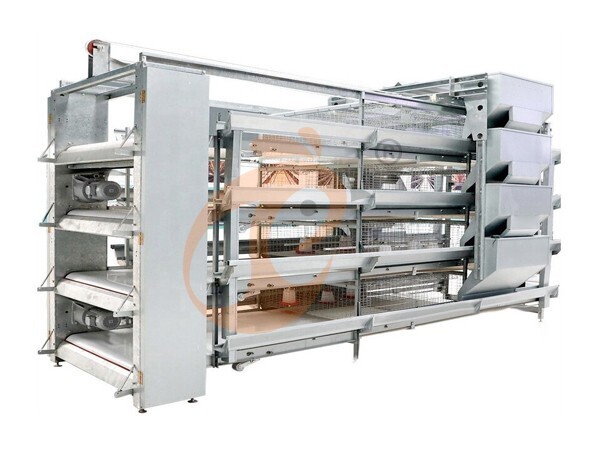
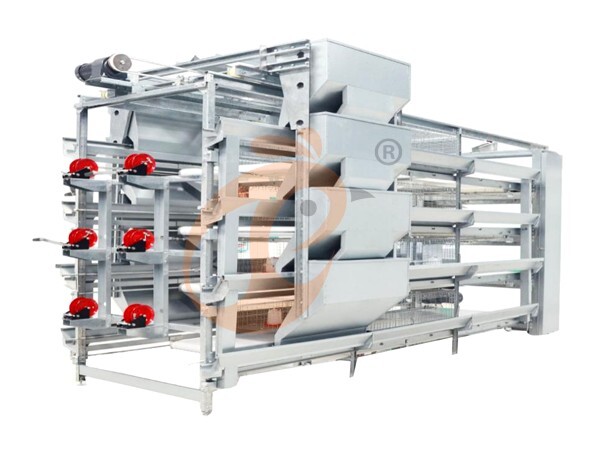
 >30,000 Pullets Automatic H Type Battery Cage1. More than 30,000 pullets a house, choose it.
2. It is designed to rearing older than 1 day old pullets to 12 to 16 weeks old chicken starting laying eggs.
3. Its lifespan is more than 25 years.
4. Its structure are Vcloud artificial intelligent fusion, electric control cabinet, automatic equipment of drinking, feeding, manure clean, manual harvesting.
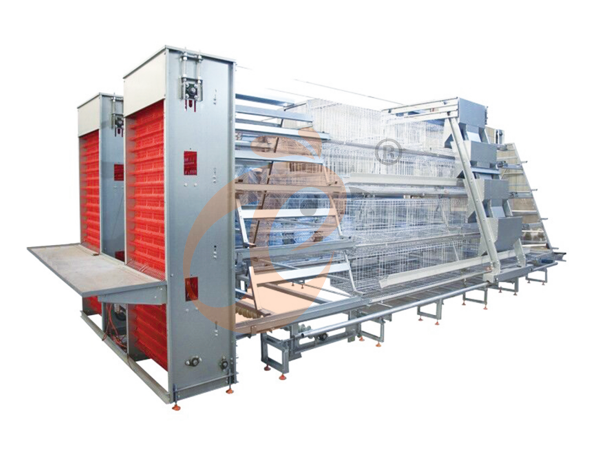
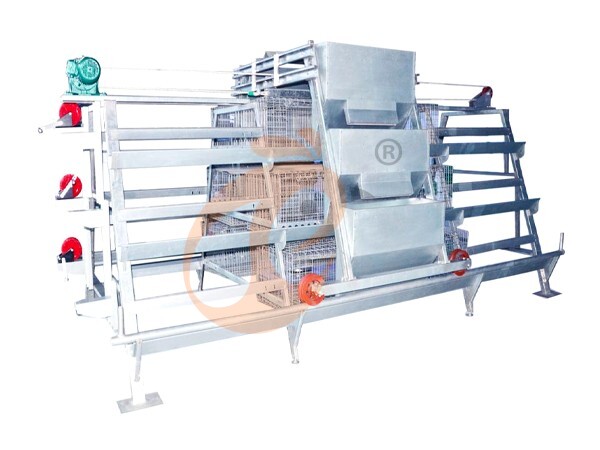
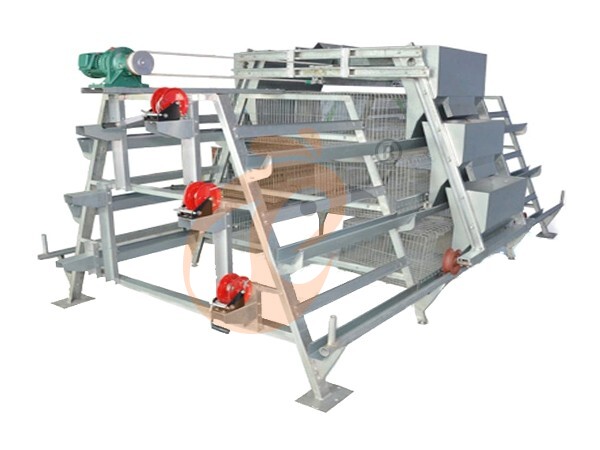
5. Our 24 hour online reception What’sApp NO. is +8618830120193 <30,000 Pullets Automatic A Type Battery Cage1. 10,000 to 30,000 pullets a house, choose it.
2. It is designed to rearing older than 1 day old pullets to 12 to 16 weeks old chicken starting laying eggs.
3. Its lifespan is more than 25 years.
4. Its structure are Vcloud artificial intelligent fusion, electric control cabinet, automatic equipment of drinking, feeding, manure clean, manual harvesting.
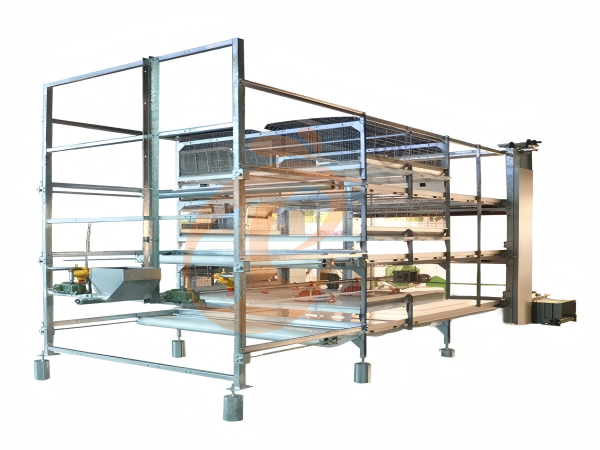
5. Our 24 hour online reception What’sApp NO. is +86 18830120193. >30,000 Broilers Semi-Automatic Harvest H Type Battery Cage1. More than 30,000 broilers a house, choose it.
2. It is designed to rearing 1 to 45 day old adult broiler ready for market.
3. Its lifespan is more than 20 years.
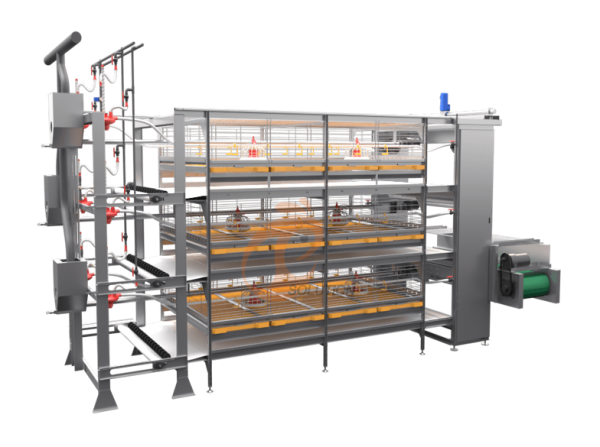
4. Our 24 hour online reception What’sApp NO. is +8618830120193, +234 8111199996. >30,000 Broilers Manual Harvest H Type Battery Cage1. More than 30,000 broilers a house, choose it.
2. It is designed to rearing 1 to 45 day old adult broiler ready for market.
3. Its lifespan is more than 20 years.
4. Its structure are Vcloud artificial intelligent fusion, electric control cabinet, automatic equipment of drinking, feeding and manure clean, manual harvesting.
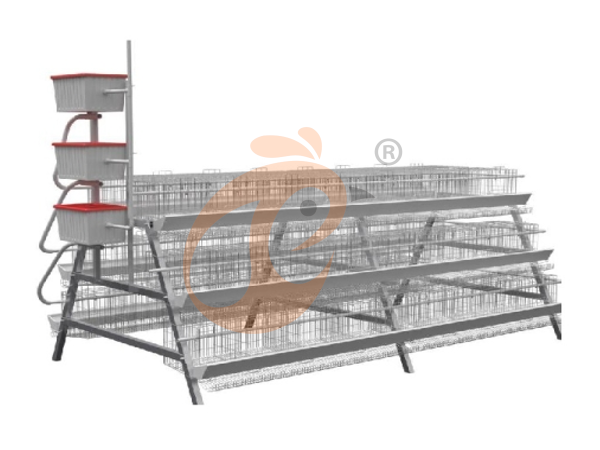
5. Our 24 hour online reception What’sApp NO. is +8618830120193, +234 8111199996. <30,000 Broilers Manual Harvest A Type Battery Cage1. Less 30,000 broilers a house, choose it.
2. It is designed to rearing 1 to 45 day old adult broiler ready for market.
3. Its lifespan is more than 20 years.
4. Its structure are Vcloud artificial intelligent fusion, electric control cabinet, automatic equipment of drinking, feeding and manure clean, manual harvesting.
5. Our 24 hour online reception What’sApp NO. is +8618830120193, +234 8111199996. HK Headquarter Offers EU-standard Poultry Farm Solutions, Manufacture Poultry Farm Equipment1. Continuous communication with the EU and the US
2. China, Nigeria, Ethiopia, Tanzania branch companies and factories
3. The products’ quality is customized for local poultry farms
4. Poultry cage and poultry farm equipment stock for sale
5. 24 online reception Whatsapp NO. : +8618830120193,contact us to get full information China Branch Offer Poultry Farm Business Plan, Manufacture Poultry Farm Equipment1. Address: Flat/RM 2416, 24/F, Runxing Building, Youyi Nan Street, Shijiazhuang City, Hebei Province, China
2. Poultry cage and poultry farm equipment factory and stock for sale
3. Customized for local poultry farms
4. Quality and design are based on Euro
5. 24 online reception Whatsapp NO. : +8618830120193 Nigeria Branch Offer Poultry Farm Business Plan, Manufacture Poultry Farm Equipment1. Address: After Sinoma Office, 200 Meters Near Danco Filling Station, Lagos/Ibadan Expressway, Lagos State, Nigeria
2. Poultry cage and poultry farm equipment factory and stock for sale
3. Customized for Nigerian poultry farms
4. Quality and design are based on Euro
5. 24 online reception Whatsapp NO. : +8618830120193 Ethiopia Branch Offer Poultry Farm Business Plan, Manufacture Poultry Farm Equipment1. Address: Gelan Gura, Akaki-kaliti Sub City, Addis Ababa, Ethiopia
2. Poultry cage and poultry farm equipment stock for sale
3. Customized for Ethiopian poultry farms
4. Quality and design are based on Euro
5. 24 online reception Whatsapp NO. : +8618830120193, contact us to get price list Tanzania Branch Offer Poultry Farm Business Plan, Manufacture Poultry Farm Equipment1. Address: No.8, Sova Road, Msufini, Mlandizi, Kibaha, Pwani, Tanzania
2. Poultry cage and poultry farm equipment factory and stock for sale
3. Customized for Tanzanian poultry farms
4. Quality and design are based on Euro
5. 24 online reception Whatsapp NO. : +8618830120193
Contact