


Blog
Battery Cage System For Layers In Africa: Feed Efficiency, Heat Management, Labour Savings And Return On Investment
For African layer farmers, the real question is not simply whether a battery cage looks modern, but whether an advantage of battery cage system can turn feed, land, labour and disease risks into measurable profit.
FAO identifies feed as the most important variable cost in poultry production, typically representing 65%–70% of total costs.
Africa is not one single poultry market. Nigeria, Ghana, Senegal, Kenya, Uganda, Tanzania, Zambia, Zimbabwe, South Africa, Egypt and Morocco face different combinations of feed inflation, heat stress, unreliable electricity, disease pressure, land scarcity and limited access to finance.
Nigeria and Senegal: Feed costs are highly sensitive to maize and soybean meal prices.
Kenya and Uganda: Feed and day-old-chick costs are major constraints for small and mid-size farms.
Tanzania, Mozambique and coastal West Africa: Humidity, heat and disease pressure require better ventilation and manure separation.
South Africa, Zambia and Zimbabwe: Commercial farms must plan for electricity reliability, labour costs and scalable production.
Egypt and Morocco: Heat management, water efficiency and intensive production require climate-controlled housing.
A practical advantage of battery cage design is its ability to standardise feed delivery, egg collection and manure removal.
In a 20,000-bird layer house consuming 2,400 kg of feed daily, preventing 1% feed waste saves 24 kg per day; at USD 0.45 per kg, the farm retains about USD 3,942 across a 365-day cycle.
European union standard reference only.
Another advantage of battery cage operations is environmental control.
A well-designed layer house should maintain airflow of approximately 2–3 m/s at bird level during hot periods, keep relative humidity below 70% where possible, and provide 0.25–0.30 litres of clean drinking water per hen per day under tropical conditions.
These parameters matter especially in Nigeria, Ghana, Tanzania, Mozambique, Egypt and Morocco.
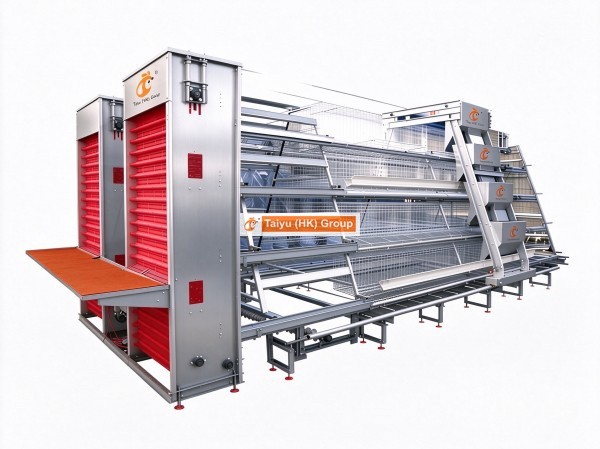
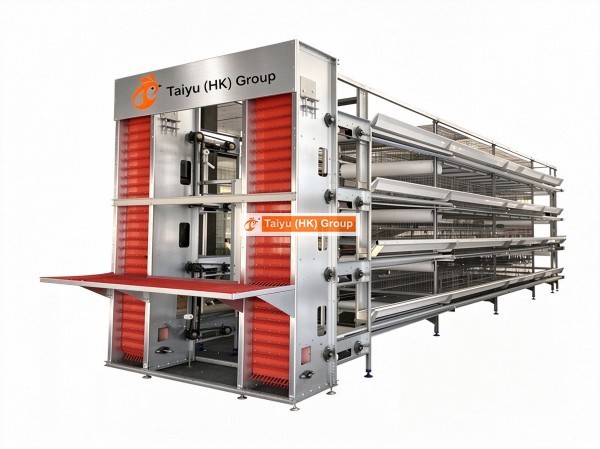
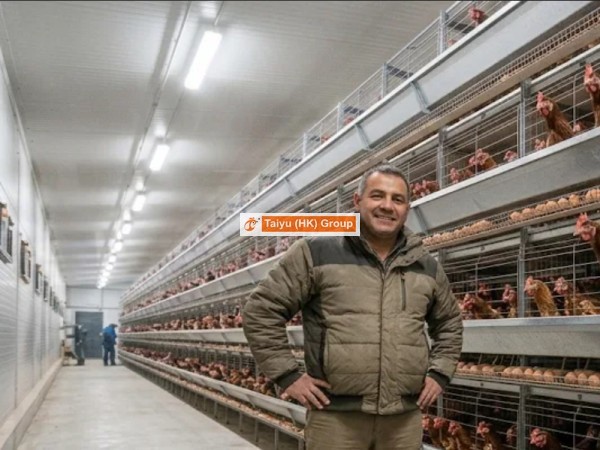
Check the popular types of chicken battery cages for sale
Learn More About Southeast Asia
Learn More About Latin America
1. Why Modern Battery Cage Systems Are Essential For African Poultry Farming
African poultry demand is rising, but traditional deep-litter and free-range systems often struggle with feed loss, wet litter, disease exposure, labour-intensive egg collection and limited expansion space.
A modern battery cage system gives African farmers a more controllable way to raise layers, especially in land-constrained urban markets such as Lagos, Nairobi, Accra, Kampala, Dar es Salaam, Lusaka and Harare.
The main advantage of battery cage systems is that they combine greater stocking density with easier feeding, egg collection, manure removal and flock monitoring.
Greater density: Multi-tier cages allow African farms to use vertical space instead of expanding horizontally.
Cleaner eggs: Eggs roll away from droppings, reducing contamination and breakage.
Less feed waste: Positioned troughs reduce feed scattering and contamination.
Easier disease control: Manure separation reduces contact with droppings and pathogens.
Better scalability: Farmers can begin with 1,000 birds and expand to 100,000+ birds in modules.
Clients:
Traditional deep litter farming in Africa causes too much feed loss and sick birds. Can a battery cage system really solve this for my local farm?
Taiyu Group (HK):
Absolutely. African climates require clean, separated environments—especially in humid coastal areas of Nigeria, Ghana, Tanzania and Mozambique, and in hot inland markets such as Burkina Faso, Mali, Niger and Chad. Are you tired of losing costly feed on the floor and treating repeated coccidiosis outbreaks?
2. Core Overview: Four Advantages For African Climate And Markets
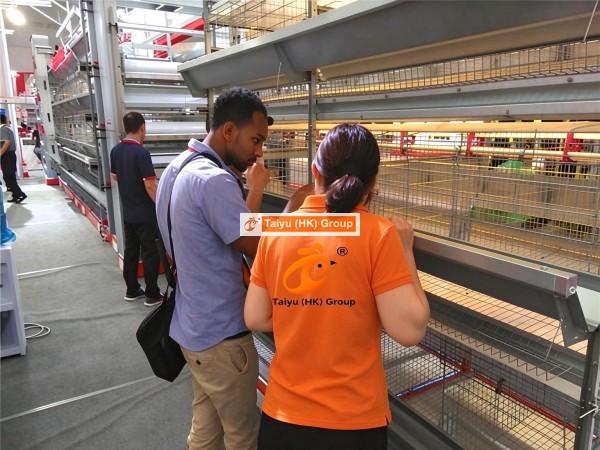
The first major advantage of battery cage systems in Africa is controlled productivity: more birds per square metre, cleaner eggs, less feed waste and easier flock management.
In Nigeria, Ghana, Kenya, Uganda, Tanzania, Zambia, Zimbabwe, South Africa, Egypt and Morocco, farmers face different input costs and climates, but all need systems that make production predictable.
A second advantage of battery cage systems is adaptability: A-type cages suit naturally ventilated sheds, while H-type systems suit larger commercial farms with mechanical ventilation and automation.
Data is for reference only. Swipe horizontally to view full table.
Advantage 1 — Greater density: More layers can be housed within the same building footprint.
Advantage 2 — Cleaner eggs: Eggs are separated from manure, improving saleable quality.
Advantage 3 — Better feed control: Positioned troughs reduce feed waste and support daily feed records.
Advantage 4 — Easier expansion: Farms can upgrade from manual A-type cages to automated H-type systems.
Clients:
How do I know battery cages will withstand Africa’s humid heat and tropical weather?
Taiyu Group (HK):
Hot-dip galvanised steel frames are designed for humid coastal and tropical African conditions, including Nigeria, Ghana, Côte d’Ivoire, Cameroon, Tanzania, Mozambique and Madagascar. Before choosing a cage, check your region’s average humidity, maximum temperature, rainfall pattern and ventilation capacity. The right advantage of battery cage design must match your local climate—not just the lowest equipment price.
Data is based on more than 20 years of after-sales follow-up records collected by Taiyu Group (HK).
3. Space And Density: Better Land Use In African Cities
A major advantage of battery cage systems is space efficiency.
In African cities where land prices are rising—such as Lagos, Nairobi, Accra, Abidjan, Dakar, Kampala, Dar es Salaam and Johannesburg—vertical cage systems allow farms to produce more eggs without buying more land.
A third advantage of battery cage systems is that multi-tier layouts make expansion possible without relocating the entire farm.
Data is for reference only. Swipe horizontally to view full table.
Nigeria: Useful for poultry projects around Lagos, Ibadan, Abeokuta and Kano, where land and logistics costs are rising.
Kenya: Suitable for peri-urban layer farms near Nairobi, Nakuru, Kisumu and Mombasa.
Ghana: Fits commercial egg producers around Accra, Kumasi and Tema.
South Africa: Useful where land, labour and electricity costs require greater output per square metre.
Clients:
Land costs in my region are rising fast. How many more birds can I fit in a 1,000 m² house in Africa?
Taiyu Group (HK):
With deep litter, many African farms reach about 5,000–6,000 birds in 1,000 m². With a properly ventilated multi-tier battery cage layout, the same building can often house 12,000–15,000 layers or more, depending on cage type, aisle width and climate-control design. This is a major advantage of battery cage systems for land-constrained farms in Nigeria, Kenya, Ghana, Uganda and South Africa.
Data is based on more than 20 years of after-sales follow-up records collected by Taiyu Group (HK).
4. Disease Control: Reduce Wet-Season Mortality
Another critical advantage of battery cage systems is biosecurity.
In African rainy seasons, deep-litter houses can become wet, ammonia-heavy and difficult to disinfect, increasing exposure to coccidiosis, worms, respiratory disease and droppings-borne pathogens.
By separating birds from manure, battery cages make cleaning and disinfection more practical; research also notes that cage systems can reduce disease risk and produce cleaner eggs.
Data is for reference only. Swipe horizontally to view full table.
Nigeria and Ghana: Wet-season management is especially important where rainfall and humidity remain elevated.
Kenya, Uganda and Tanzania: Cage systems can support cleaner housing where litter quality and disease pressure vary by season.
South Africa and Namibia: Biosecurity remains essential even in drier climates, particularly around commercial supply chains.
Clients:
Outbreaks like coccidiosis destroy African layer farms every rainy season. Will cages stop this?
Taiyu Group (HK):
In battery cages, hens are separated from droppings, and automated manure belts or scraper systems remove waste regularly. This does not replace vaccination, disinfection or dry-house management, but it is a major advantage of battery cage systems for farms in Nigeria, Ghana, Côte d’Ivoire, Cameroon, Tanzania and Mozambique during wet seasons.
Data is based on more than 20 years of after-sales follow-up records collected by Taiyu Group (HK).
4. Feed Conversion And Egg Quality: Reduce Waste And Breakage
The most financial advantage of battery cage systems is feed control.
Because feed represents 65%–70% of poultry production costs, even a small reduction in waste can materially improve profit in feed-importing African markets such as Nigeria, Ghana, Senegal, Kenya, Uganda, Zambia and Zimbabwe.
A further advantage of battery cage systems is cleaner egg collection: sloped cage floors move eggs away from droppings and reduce breakage.
Data is for reference only. Swipe horizontally to view full table.
Nigeria and Senegal: Maize-based feed costs make waste reduction a direct profit lever.
Kenya and Uganda: Feed and chick costs make feed efficiency essential for smaller farms.
Zambia and Zimbabwe: Feed availability and price volatility make controlled feeding more valuable.
Clients:
Feed prices in Africa are extremely expensive right now. How does the cage design actually save feed?
Taiyu Group (HK):
A deep trough with anti-spill edges keeps feed inside the trough instead of on the floor. Combined with correct feeding height, measured daily feed allocation and clean drinking water, this is a practical advantage of battery cage systems for African farms facing volatile maize and soybean meal prices.
5. Scalability: From 1,000 To 100,000+ Layers
A decisive advantage of battery cage systems is scalability.
African farms should not use the same configuration at 1,000, 10,000 and 100,000 birds; the correct system depends on land, power, labour, capital and market demand.
A further advantage of battery cage systems is modular expansion: a farm can start with manual A-type cages and later upgrade to automated H-type systems as production grows.
Data is for reference only. Swipe horizontally to view full table.
1,000–2,000 birds: Best for new farmers in Kenya, Uganda, Tanzania, Zambia and Zimbabwe that need a measured entry point.
5,000–10,000 birds: Suitable for growing farms in Nigeria, Ghana, Côte d'Ivoire, Cameroon and Senegal.
20,000–50,000 birds: Best for commercial projects near Lagos, Accra, Nairobi, Lusaka and Johannesburg.
100,000+ birds: Requires industrial planning for power, ventilation, manure treatment, logistics and biosecurity.
Clients:
I want to scale my farm in Nigeria from 2,000 to 20,000 layers. Will labour management become a nightmare?
Taiyu Group (HK):
Not if the project is designed in stages. At 2,000 birds, A-type cages with manual collection may be enough; at 20,000 birds, automatic drinkers, mechanical manure removal and semi-automatic egg collection reduce daily labour sharply. This staged approach is a major advantage of battery cage systems for Nigerian, Ghanaian, Kenyan and Zambian farms that need to grow without over-investing too early.
Data is based on more than 20 years of after-sales follow-up records collected by Taiyu Group (HK).
6. A-Type Vs H-Type: Choosing The Right African Cage
Another practical advantage of battery cage systems is that African farmers can choose between A-type and H-type configurations according to shed design, power reliability and expansion plans.
A-type cages are generally easier to install and manage in naturally ventilated houses; H-type cages suit dense commercial projects that can support ventilation, automation and maintenance.
The right advantage of battery cage choice is therefore not the most expensive cage, but the one that matches local conditions.
Data is for reference only. Swipe horizontally to view full table.
Clients:
Should I choose A-type or H-type cages for my farm in Ghana or Kenya?
Taiyu Group (HK):
Choose A-type if you have a naturally ventilated shed, limited power reliability and a first-stage capacity below 20,000 birds. Choose H-type if you plan 20,000+ layers, have reliable ventilation and power backup, and need reduced labour per bird. Matching cage type to local conditions is a key advantage of battery cage system design.
7. Housing Systems And Management Requirements
African layer farms can use free-range, deep-litter floor systems, slatted-floor systems or battery cage systems.
FAO describes deep litter as a confined system using 3–4 birds/m² with a 5–10 cm litter layer, while slatted floors can support about five birds/m²; battery cages are mainly used for laying birds and involve greater initial capital investment.
Data is for reference only. Swipe horizontally to view full table.
For a 10,000-layer project, a deep-litter house may require roughly 1,700–2,000 m² of floor area, while a battery cage layout may require about 500–850 m².
The cage option therefore suits urban and peri-urban producers in Lagos, Accra, Nairobi, Kampala and Johannesburg where land availability is limited.
European union standard reference only.
8. Frequently Asked Questions: Battery Cage Systems In Africa
Data is for reference only. Swipe horizontally to view full table.
9. Taiyu (HK) Group - One Of China Toppest Battery Cage System Exporter
1. Global Service Network
Headquartered in Hong Kong, with branches and factories in China, Vietnam, Thailand, Nigeria, Kenya, Ethiopia, and Tanzania, providing more localized project and after-sales support.
2. International Quality Standards
Strict quality control and double inspections. Certifications and export documents include CE, SGS, ISO 9001, CCVO, PVOC, SONCAP, COC, ECTN, FORM A/F/M, and more.
3. One-to-One VIP Service
Dedicated account managers provide customized farm designs, equipment configurations, and quotations for projects ranging from 500 to 100,000+ birds per house.
4. Lifetime After-Sales Service
Installation guidance, equipment commissioning, operator training, remote technical support, spare parts supply, and ongoing maintenance.
10. Contact Us To Received Your Customized Poultry Farm Plan
Headquarters And Branchs
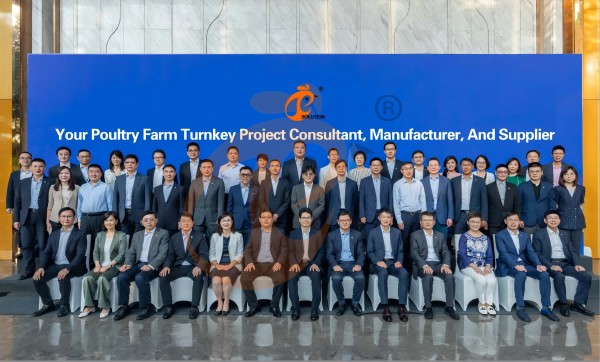
Hong Kong Headquarter Management Team
Hong Kong Headquarter Taiyu Industrial Group CO., LTD
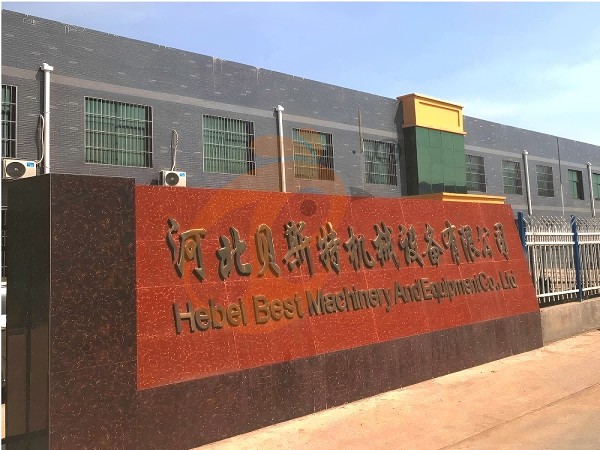
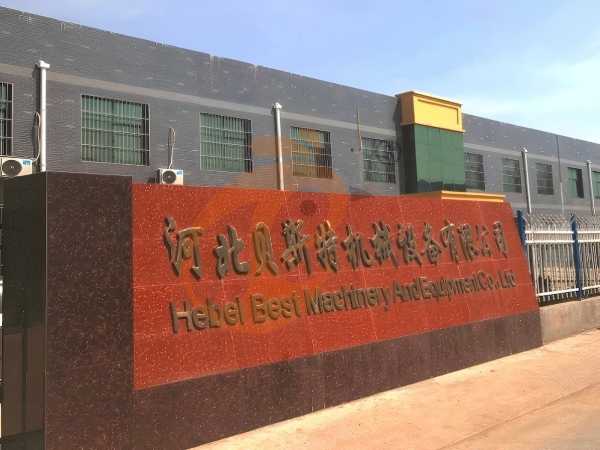
China Hebei Best Machinery And Equipment CO., LTD
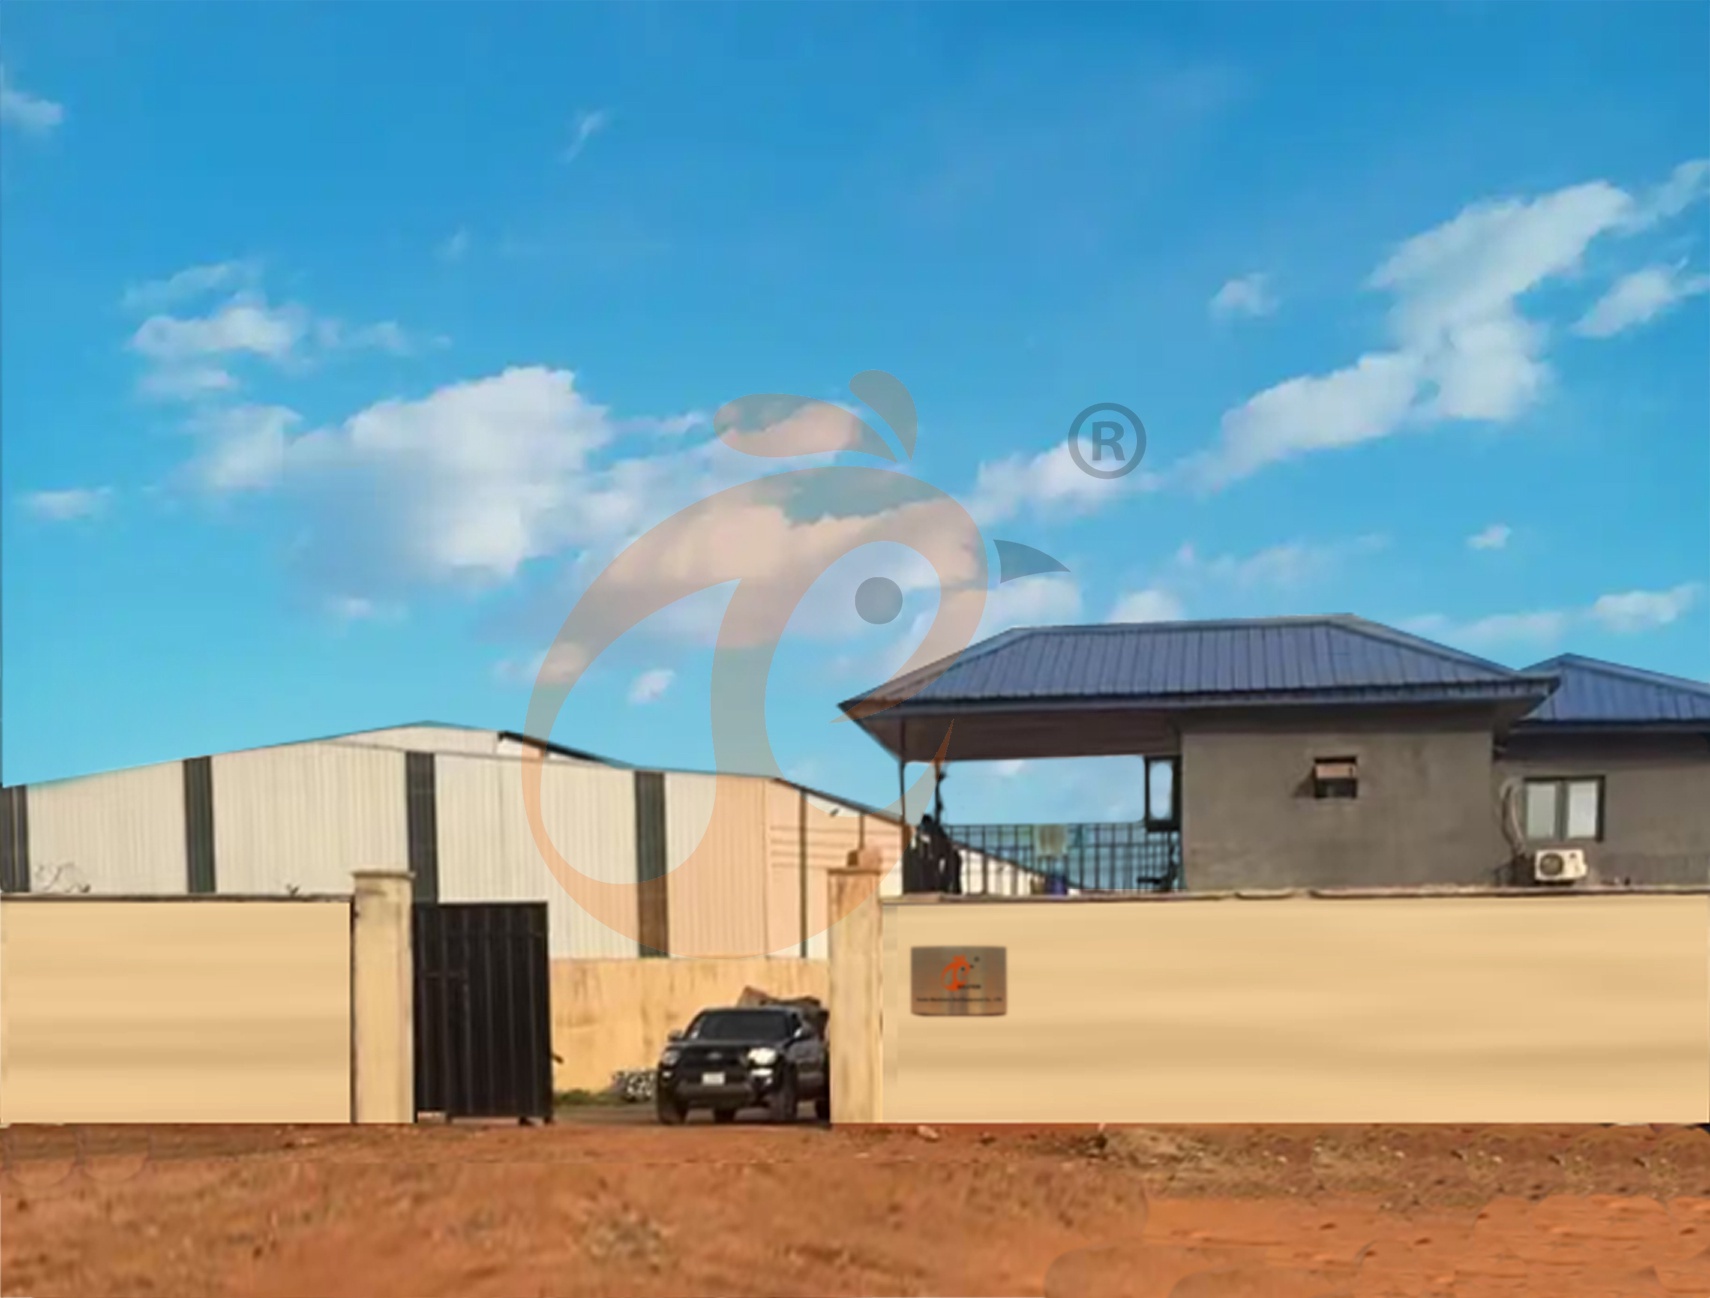
Nigeria Vanke Machinery And Equipment CO., LTD
Tanzania Best Machinery And Equipment CO., LTD
Ethiopia Best Hebei Machinery Manufacturing PLC
Reception /24 WhatsApp NO. : +8618830120193
FAQ
Message
Products recommended
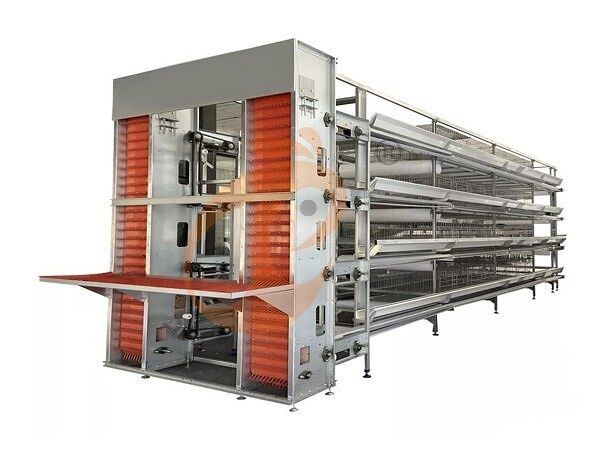
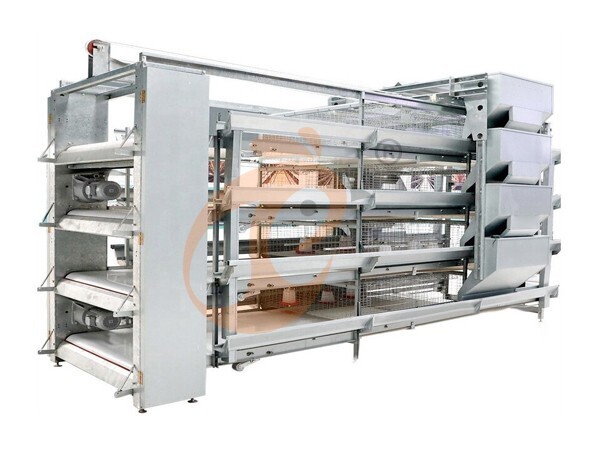
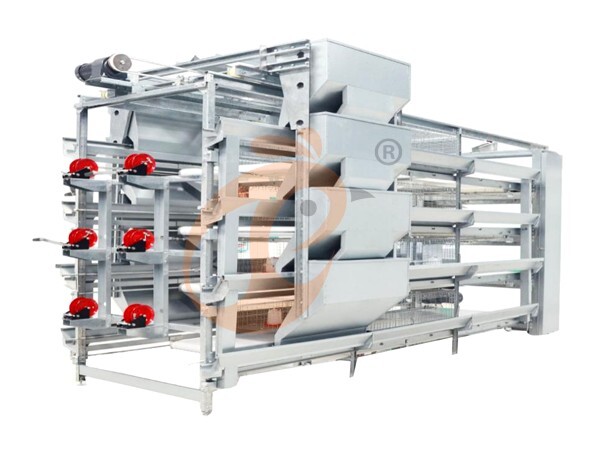
 Automatic H Type Battery Cage System1. For 30,000–1,000,000+ layer farmers.
2. Contains 30,000-100,000 chickens a house.
3. Makes feed utilization >98%, egg production rate 96%-99%, egg broken rate<0.3%.
4. Certificate: CE, SGS, PC, ISO 9001, SONCAP, PVOC,COC, OC, FORM M/A/F, CO and so on .
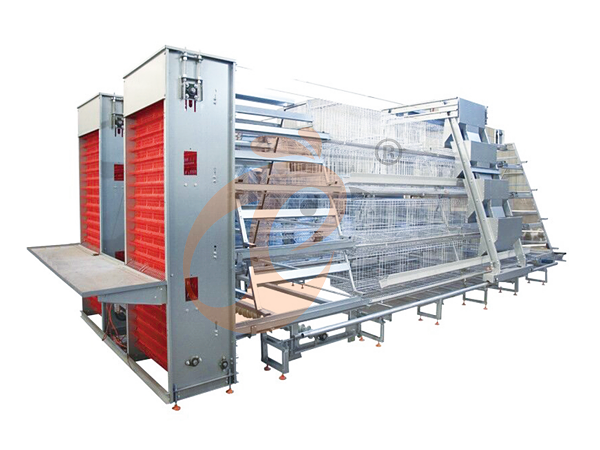
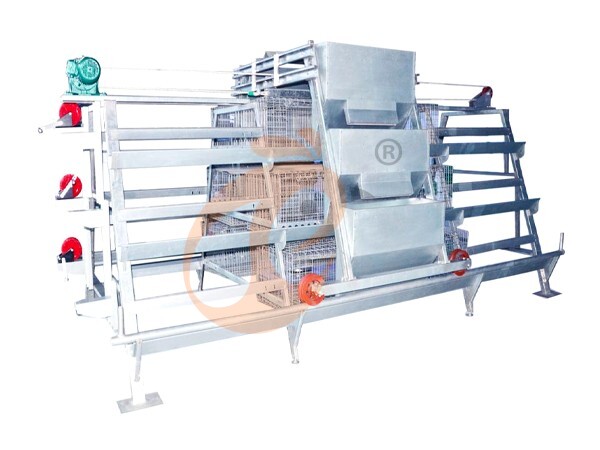
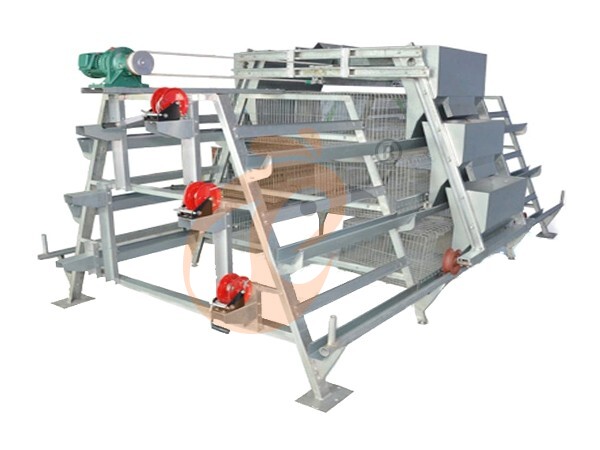
5. 24-hour online support: What'sApp +8618830120193. Automatic A Type Battery Cage For Layers1. For 5,000–30,000+ layer farmers.
2. Contains 30,000-100,000 chickens a house.
3. European standard automatic A type battery cage for layers.
4. Certificate: CE, SGS, PC, ISO 9001, SONCAP, PVOC,COC, OC, FORM M/A/F, CO and so on .
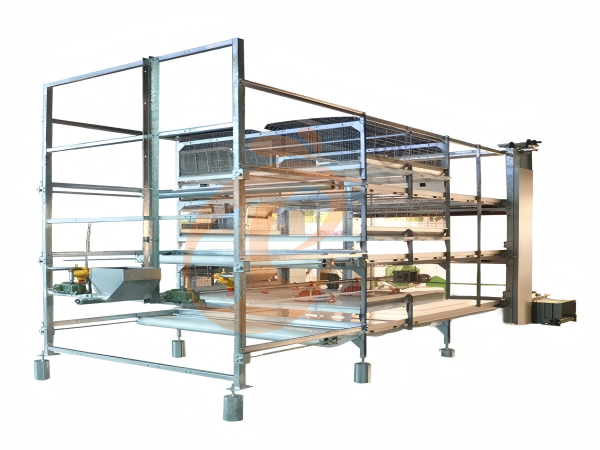
5. 24-hour online support: What'sApp +8618830120193. >30,000 Pullets Automatic H Type Battery Cage1. More than 30,000 pullets a house, choose it.
2. It is designed to rearing older than 1 day old pullets to 12 to 16 weeks old chicken starting laying eggs.
3. Its lifespan is more than 25 years.
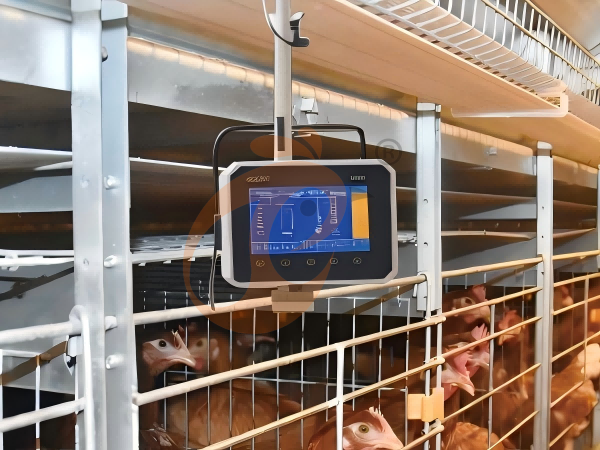
4. Its structure are Vcloud artificial intelligent fusion, electric control cabinet, automatic equipment of drinking, feeding, manure clean, manual harvesting.
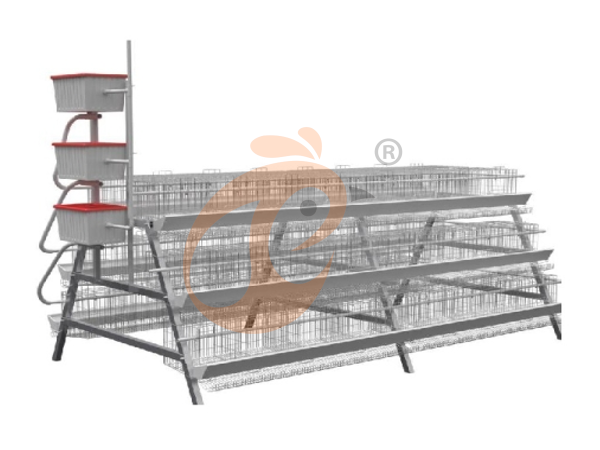
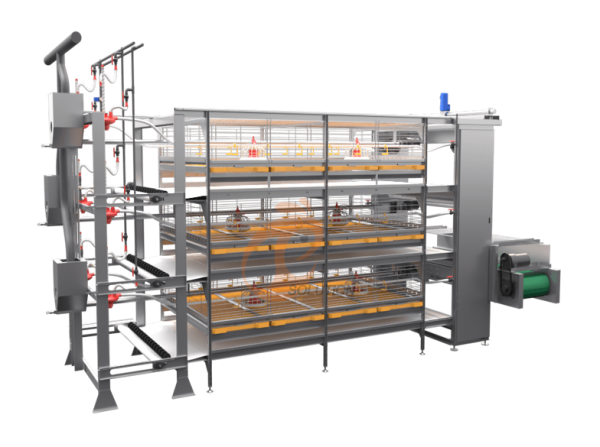
5. Our 24 hour online reception What’sApp NO. is +8618830120193 <30,000 Pullets Automatic A Type Battery Cage1. 10,000 to 30,000 pullets a house, choose it.
2. It is designed to rearing older than 1 day old pullets to 12 to 16 weeks old chicken starting laying eggs.
3. Its lifespan is more than 25 years.
4. Its structure are Vcloud artificial intelligent fusion, electric control cabinet, automatic equipment of drinking, feeding, manure clean, manual harvesting.
5. Our 24 hour online reception What’sApp NO. is +86 18830120193. >30,000 Broilers Semi-Automatic Harvest H Type Battery Cage1. More than 30,000 broilers a house, choose it.
2. It is designed to rearing 1 to 45 day old adult broiler ready for market.
3. Its lifespan is more than 20 years.
4. Our 24 hour online reception What’sApp NO. is +8618830120193, +234 8111199996. >30,000 Broilers Manual Harvest H Type Battery Cage1. More than 30,000 broilers a house, choose it.
2. It is designed to rearing 1 to 45 day old adult broiler ready for market.
3. Its lifespan is more than 20 years.
4. Its structure are Vcloud artificial intelligent fusion, electric control cabinet, automatic equipment of drinking, feeding and manure clean, manual harvesting.
5. Our 24 hour online reception What’sApp NO. is +8618830120193, +234 8111199996. <30,000 Broilers Manual Harvest A Type Battery Cage1. Less 30,000 broilers a house, choose it.
2. It is designed to rearing 1 to 45 day old adult broiler ready for market.
3. Its lifespan is more than 20 years.
4. Its structure are Vcloud artificial intelligent fusion, electric control cabinet, automatic equipment of drinking, feeding and manure clean, manual harvesting.
5. Our 24 hour online reception What’sApp NO. is +8618830120193, +234 8111199996. HK Headquarter Offers EU-standard Poultry Farm Solutions, Manufacture Poultry Farm Equipment1. Continuous communication with the EU and the US
2. China, Nigeria, Ethiopia, Tanzania branch companies and factories
3. The products’ quality is customized for local poultry farms
4. Poultry cage and poultry farm equipment stock for sale
5. 24 online reception Whatsapp NO. : +8618830120193,contact us to get full information China Branch Offer Poultry Farm Business Plan, Manufacture Poultry Farm Equipment1. Address: Flat/RM 2416, 24/F, Runxing Building, Youyi Nan Street, Shijiazhuang City, Hebei Province, China
2. Poultry cage and poultry farm equipment factory and stock for sale
3. Customized for local poultry farms
4. Quality and design are based on Euro
5. 24 online reception Whatsapp NO. : +8618830120193 Nigeria Branch Offer Poultry Farm Business Plan, Manufacture Poultry Farm Equipment1. Address: After Sinoma Office, 200 Meters Near Danco Filling Station, Lagos/Ibadan Expressway, Lagos State, Nigeria
2. Poultry cage and poultry farm equipment factory and stock for sale
3. Customized for Nigerian poultry farms
4. Quality and design are based on Euro
5. 24 online reception Whatsapp NO. : +8618830120193 Ethiopia Branch Offer Poultry Farm Business Plan, Manufacture Poultry Farm Equipment1. Address: Gelan Gura, Akaki-kaliti Sub City, Addis Ababa, Ethiopia
2. Poultry cage and poultry farm equipment stock for sale
3. Customized for Ethiopian poultry farms
4. Quality and design are based on Euro
5. 24 online reception Whatsapp NO. : +8618830120193, contact us to get price list Tanzania Branch Offer Poultry Farm Business Plan, Manufacture Poultry Farm Equipment1. Address: No.8, Sova Road, Msufini, Mlandizi, Kibaha, Pwani, Tanzania
2. Poultry cage and poultry farm equipment factory and stock for sale
3. Customized for Tanzanian poultry farms
4. Quality and design are based on Euro
5. 24 online reception Whatsapp NO. : +8618830120193
Contact